United States wearable-strap RFQ desk · no public hotline EN
Liquid silicone injection molding cold-runner tool
Factory matching · LSR strap overmold

liquid silicone injection molding manufacturers

Build one wearable RFQ so liquid silicone injection molding manufacturers price the same strap revision, flash rule, post-cure hours, T1 count, and Incoterm. This desk ranks replies; it does not run a LIM press.

ISO 9001 to request ISO 13485 to request IATF 16949 to request FDA file to request RoHS / REACH to request

How a comparable LSR strap request is built

The sequence is a buyer checklist for wearable overmolds, not a factory history. Oven charts and cavity counts stay with the supplier that writes them.

01

Lock the revision

Name the strap STEP and 2D files, the buckle datum scheme, and whether flash is allowed at the parting line that sits against skin. If a redline exists, date it so every liquid silicone injection molding manufacturers reply cites the same paper.
02

State chemistry and post-cure

Write LSR grade, Shore A, pigment, and the post-cure cycle written on the traveler. If HCR is still an option, treat it as a second row, not a silent swap inside the LSR cell.

03

Split the cost buckets

Ask each plant to quote NRE / MUD or steel tooling, piece price, deflash, peel testing, oven hours, and freight as separate lines. A blended strap number hides which scope was dropped.

04

Line up landed totals

Convert currency, add duties if the Incoterm leaves them out, and keep quotation validity visible. This site does not publish a savings percentage against an unnamed market.

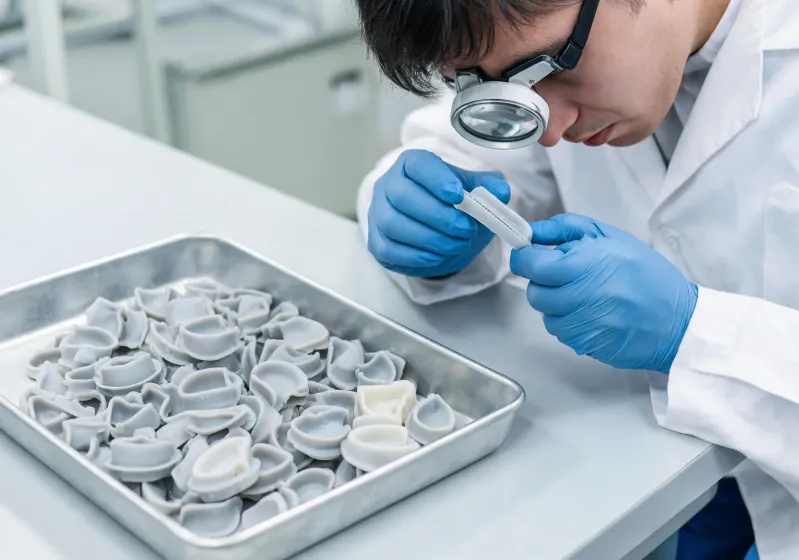
LSR flash inspection under magnification

What every supplier must quote

Each liquid silicone injection molding manufacturers package should name tool class, cavity count assumption, cold-runner versus cold-sprue, T0/T1 strap count, FAI fields, peel-test method, traveler post-cure hours, packing, and the Incoterm. If a plant omits gate vestige on the skin face, treat that as an open cosmetic risk, not a free upgrade.

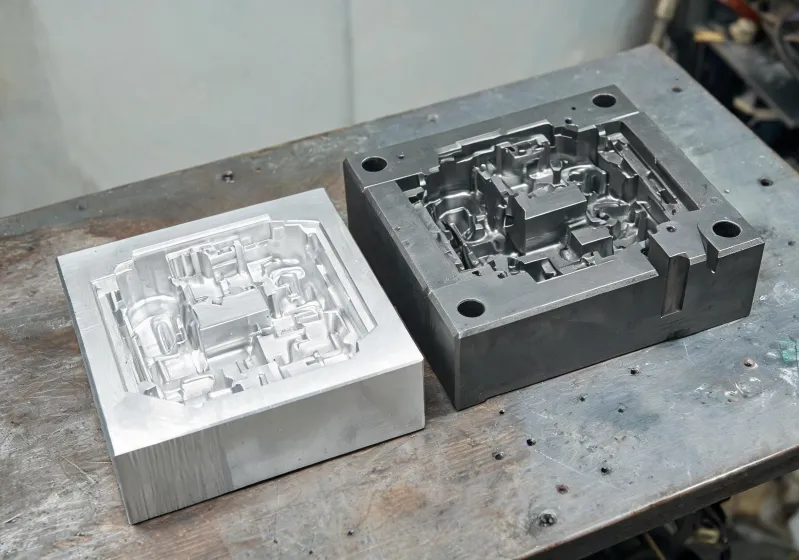
Tooling steel versus aluminum comparison

Costs and exclusions to confirm

Soft tooling advocates accept a shorter shot life to reach a wearable T1 faster. Steel tooling advocates accept a larger NRE when EAU and buckle-flash control dominate. Neither side is this desk’s preference. Ask whether texture, secondary deflash, post-cure ovens, ISO 13485 lots, and DDP freight sit inside or outside the quoted number.

RFQ lines grouped for strap comparison

GroupAsk each plant to state
GeometryRevision, draft angle, parting line, gate location, knit-line and sink-mark limits on the strap face
MaterialLSR or HCR, Shore A, pigment, post-cure cycle written on the traveler
ToolingAluminum / MUD / steel, assumed shot life, cavity count, cold-runner yes/no
QuantityT0/T1 wearable shots, first production lot, EAU, MOQ if the plant has one
InspectionFAI, CMM, CoC, Shore after oven, peel test, PPAP level if automotive-adjacent
CommercialCurrency, NRE, piece price, packing, Incoterm, destination, validity

Documents to request from a plant, not from this desk

ISO 9001

Ask for the current certificate scope and site address. A logo on a website is not a file.

ISO 13485

Needed only when the wearable file requires a medical QMS. Confirm the LSR cell you will use is in scope.

IATF 16949

Use when PPAP and Cpk on sealing or buckle features will be part of the award.

Skin-contact file

Request the compound letter and processing declaration. This desk does not hold those files.

Service desk questions

Revision, LSR or HCR, Shore A, tooling class, T1 count, peel method, post-cure hours on the traveler, packing, and Incoterm. Missing lines become exclusions.

NRE, texture, deflash, oven post-cure, extra FAI, special packing, freight, and duties unless the Incoterm includes them.

No. High-end, mid-range, or budget is a buyer trade-off for a wearable strap, not a completed audit of liquid silicone injection molding manufacturers.

Continue to the RFQ form